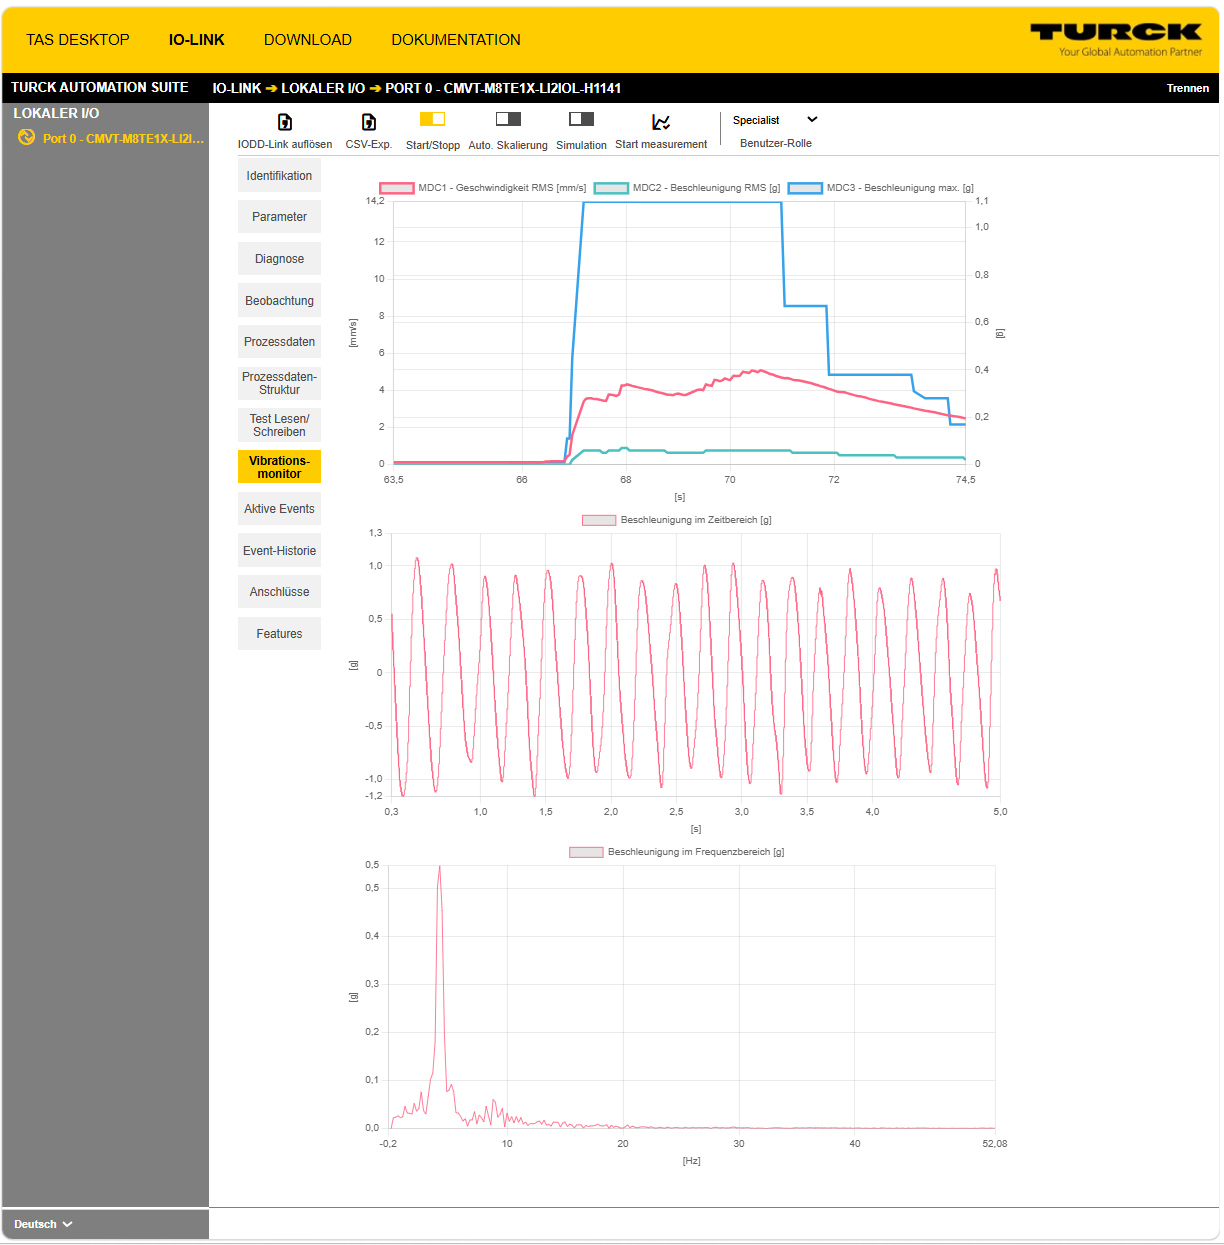
Everything at a glance: the vibration monitor in the TURCK Automation Suite (TAS) shows the cyclic characteristic values at the top, the raw acceleration data read out via BLOB transfer in the time domain in the middle, and its FFT in the frequency domain at the bottom
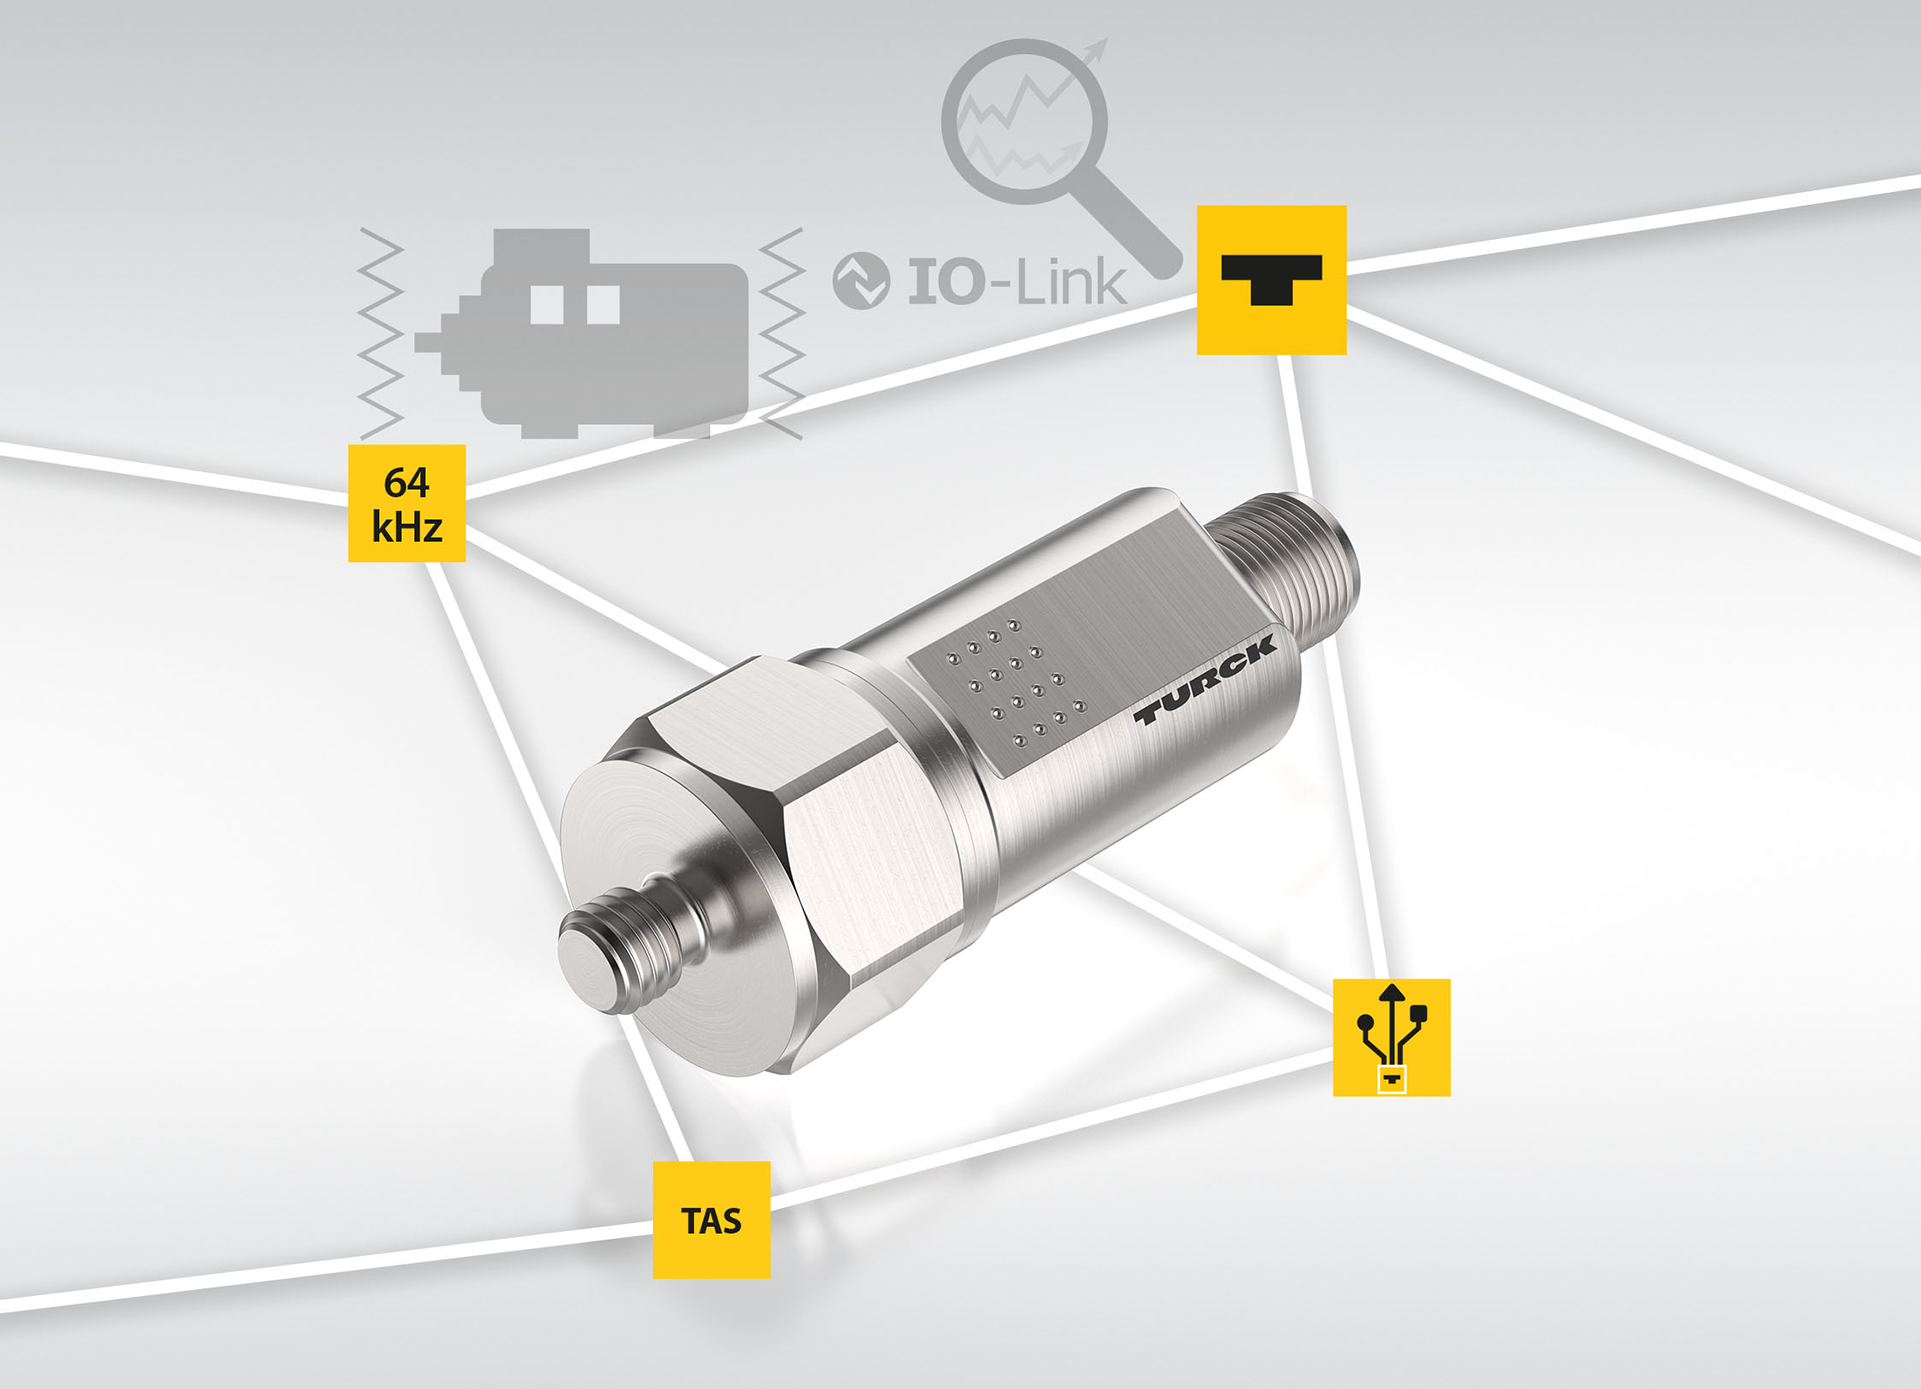
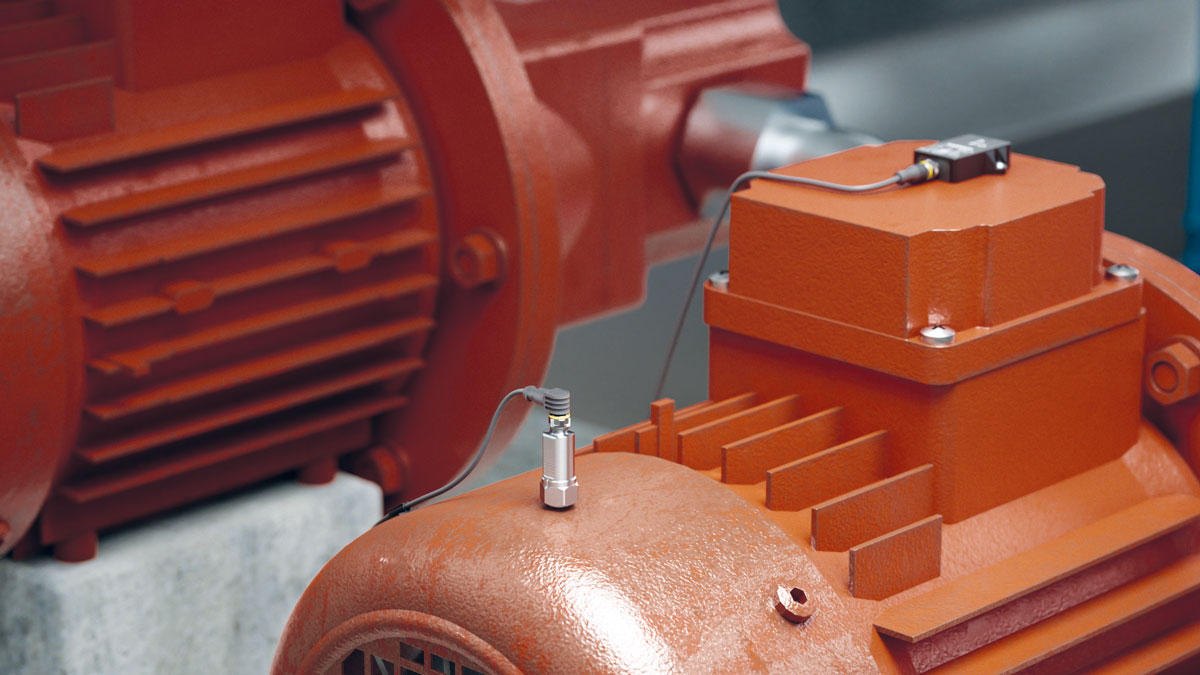
Whether it’s a drive, gearbox, pump, or fan: rotating machinery often signals an impending failure long before it happens – through changing vibration patterns. Until now, sensors typically reduced that signal to a single, compressed threshold value, leaving the actual cause – imbalance, misalignment, or an early bearing fault – a mystery. The CMVT-M8TE takes it a step further: instead of condensing everything into one limit value internally, the sensor outputs the raw acceleration data from its MEMS measuring cell via the IO-Link specification’s BLOB transfer.
That’s made possible by a sampling rate of up to 64 kHz. Each recording transfers up to 320,000 samples – enough data depth to pinpoint the cause of a vibration rather than just register that one exists. The CMVT-M8TE also provides a bearing condition indicator per DIN ISO 13373-3.
One-Click Frequency Analysis
To make the raw data usable without separate analysis software, TURCK has built BLOB transfer and FFT calculation directly into the vibration monitor of the free TURCK Automation Suite (TAS).